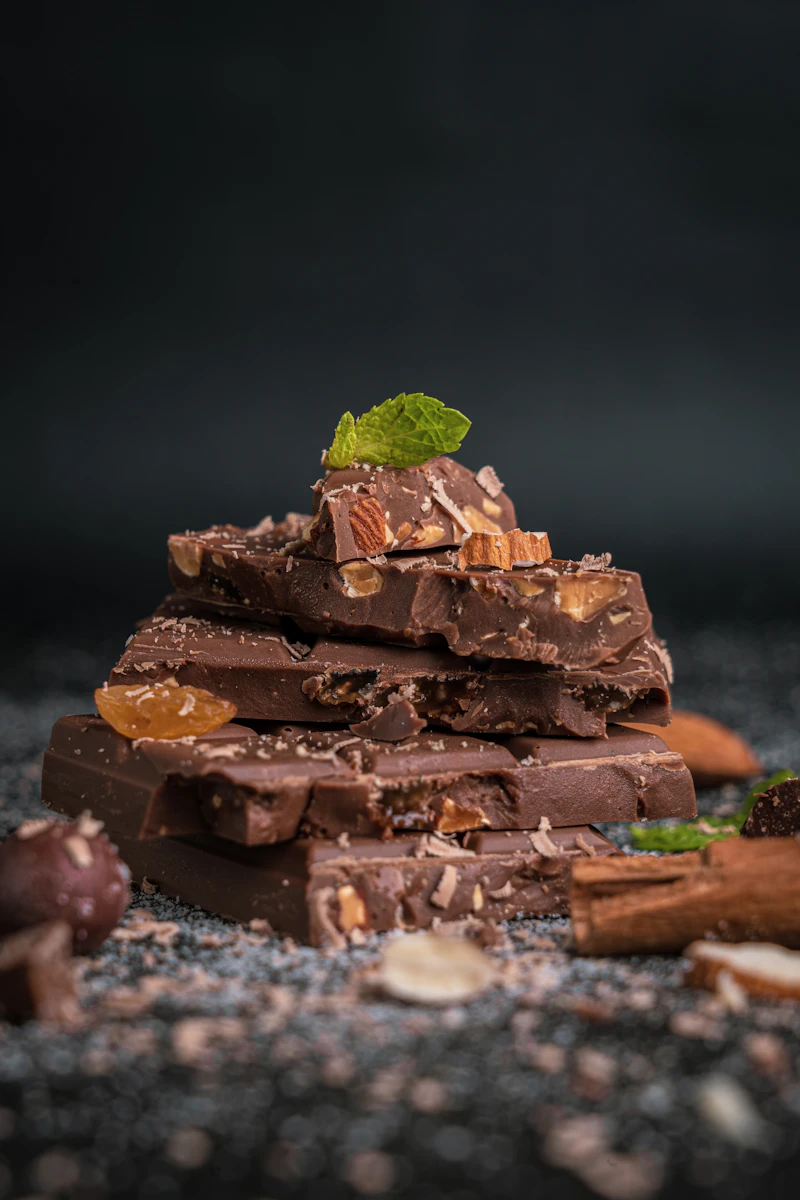
Dark Velvet Hazelnut Bar
Stone-ground West African dark cocoa folded with 22% whole roasted Giresun hazelnuts. Offers a crisp snap, intense cocoa aroma, and low sugar index for health-conscious retail segments.
An exhaustive commercial handbook for international confectionery buyers, retail importers, category managers, and private-label distributors seeking high-margin Nutty Chocolate Bars with verified shelf stability, precision roasting, and zero-defect export packaging.
As consumer preferences shift toward premium texture contrast, plant-based fat inclusions, and functional indulgence, Nutty Chocolate Bars have emerged as the fastest-growing segment in the international confectionery trade.
For global procurement teams, sourcing Nutty Chocolate Bars is no longer merely a matter of placing a commodity purchase order. AI-driven search models and user intent analytics reveal that professional buyers frequently ask technical questions regarding lipid migration, cocoa butter crystal phase stabilization, nut moisture control, fat bloom resistance during transit, and Halal-certified cross-contamination controls. To secure high retail velocities and defend shelf margins, buyers require a manufacturing partner capable of providing verifiable information gain across sensory engineering, thermal stability, and supply chain transparency.
Candy House (Private) Limited operates a state-of-the-art manufacturing facility in Lahore, Pakistan, specifically calibrated to resolve these operational challenges. By integrating dry-roasting technology, conching machinery, and climate-controlled tempering halls under one roof, we supply private-label importers across the GCC, Europe, Southeast Asia, and North America with export-grade Nutty Chocolate Bars tailored to regional sweetness profiles and transit conditions.
The primary technical hurdle in manufacturing premium nut-studded chocolate bars is moisture migration from the roasted nut kernel into the cocoa matrix, which accelerates oxidation and causes fat bloom. Candy House solves this through a proprietary double-roast thermal drying protocol that maintains nut moisture strictly below 2.5%, coupled with a precise Beta-V crystal seed tempering technique that locks cocoa butter structures even during warm-climate transport.
Our chocolate hall processes 250 kg/day of conched chocolate combined with whole, diced, or caramelized premium nuts. Explore our core export configurations below.
Stone-ground West African dark cocoa folded with 22% whole roasted Giresun hazelnuts. Offers a crisp snap, intense cocoa aroma, and low sugar index for health-conscious retail segments.
Creamy milk chocolate infused with caramelized California almond slivers and sea salt. Engineered for high impulse sales in supermarket checkout lanes and convenience retail chains.
Pure cocoa butter white chocolate blended with raw Sicilian pistachio kernels and toasted cardamom. A luxury SKU designed for duty-free shops and high-end gifting hampers.
Standard export metrics for commercial planning and container consolidation.
| Formulation Variant | Nut Inclusions | Nut Ratio (%) | Water Activity (Aw) | Shelf Life | Standard Packaging | MOQ (kg) |
|---|---|---|---|---|---|---|
| Dark Chocolate Roasted Hazelnut | Whole Hazelnuts | 20% - 25% | < 0.35 | 12 Months | Foil Inner + 250gsm Board Sleeve | 500 kg |
| Milk Chocolate Almond & Caramel | Slivered Almonds | 18% - 22% | < 0.38 | 12 Months | Flow-wrap Nitrogen Sealed Pack | 500 kg |
| White Chocolate Pistachio Silk | Whole Pistachios | 15% - 20% | < 0.32 | 9 Months | Rigid Box / Window Tin Packaging | 300 kg |
| Sugar-Free Dark Pecan (Maltitol) | Pecan Pieces | 20% | < 0.30 | 12 Months | Pharmacy-Grade Barrier Pouch | 300 kg |
| Mixed Nut Festive Slab (Custom) | Hazelnut, Almond, Cashew | 25% - 30% | < 0.36 | 12 Months | Display Carton / Gift Box | 500 kg |
Analyzing shifting supply chains, ingredient innovations, and consumer purchasing habits shaping the B2B chocolate landscape over the next decade.
Global cocoa bean prices have experienced unprecedented historic surges due to adverse weather and crop yields in West Africa. In response, forward-thinking confectionery buyers are aggressively expanding their Nutty Chocolate Bars portfolios. By increasing high-grade, dry-roasted nut inclusions (from 15% up to 30%), brand owners achieve a premium crunchy texture while reducing total cocoa mass dependence. This strategy stabilizes unit costs without sacrificing perceived retail value.
Regulatory bodies in the EU and North America are tightening restrictions on ultra-processed oils and trans-fats. International buyers now demand dry-roasted nuts that are free from oil-baths. Candy House utilizes hot-air fluid bed roasters that roast nuts in their natural oils, enhancing nut crunchiness, preventing off-flavors, and fulfilling strict clean-label standards for private-label retail lines.
Consumer search intent shows exponential growth for sugar-reduced, keto-friendly, and protein-boosted confectionery. Nutty Chocolate Bars serve as a natural carrier for functional benefits. Combining 70% dark cocoa with naturally protein-dense almonds, walnuts, and pecans allows brands to position products in both the indulge and health-and-wellness aisles. We formulate with maltitol, isomalt, and erythritol to deliver indulgence with zero added sugar.
As global temperatures rise, maintaining chain-of-custody for chocolate exports requires advanced thermal engineering. Importers are increasingly prioritizing suppliers who offer heat-stabilized cocoa formulations and eco-friendly mono-material flexible packaging that complies with emerging EPR (Extended Producer Responsibility) directives in Europe and the Gulf.
How state-of-the-art processing technology elevates product quality, shelf life, and sensory consistency.
Modern nut handling requires automated optical sorting and X-ray inspection systems to eliminate shell fragments, foreign materials, and broken kernels before entering the chocolate depositor. Candy House enforces multi-stage sorting for every nut batch.
Achieving a glossy finish and audible snap demands tight control over cocoa butter crystal polymorphism. Continuous tempering units inject Form V crystals into the liquid chocolate mix prior to nut inclusion, ensuring thermal stability during shipping.
Atmospheric oxygen degrades nut oils over time, causing rancidity. Modern flow-wrapping equipment replaces ambient oxygen with inert nitrogen gas inside aluminum foil laminate wraps, extending freshness up to 12 full months.
Operating from our primary manufacturing site at 31-Km Ferozpur Road, Lahore, Pakistan, Candy House (Private) Limited provides international buyers with a direct manufacturing model that bypasses expensive broker markups while offering technical formulation support.
We combine small-batch agility with large-scale export capabilities. Our in-house team of food technologists, confectioners, and packaging specialists manage every step from raw cocoa roasting to finished container loading.
Clear, technical, and commercial answers to aid international sourcing officers and private-label brand managers.
Nut rancidity is caused by oxidation when unsaturated fatty acids in nuts react with light, heat, and moisture. At Candy House, we mitigate this by dry-roasting nuts to a internal moisture content under 2.5%, immediately coating them in protective cocoa butter, and utilizing aluminum foil barrier films flushed with food-grade nitrogen gas during flow-wrapping. Every lot undergoes Peroxide Value (PV) testing prior to dispatch.
Our standard minimum order quantity for private label OEM Nutty Chocolate Bars is 500 kg per SKU recipe. For new buyers testing market acceptance, we offer trial orders starting at 200 kg. We also support multi-category container consolidation, allowing you to combine chocolate bars with gummies, hard candies, or marshmallows in a single shipment.
Allergen management is fundamental to our HACCP framework. We maintain segregated storage for hazelnuts, almonds, pecans, and pistachios. Roasting, chopping, and dosing are performed in designated processing cycles, followed by validated CIP (Clean-in-Place) line washdowns and swab testing before running nut-free or distinct nut formulations.
Yes. For exports destined for Middle Eastern, African, or tropical Asian regions, we optimize the cocoa butter fat crystal network through high-shear conching and specialized thermal conditioning. This allows our Nutty Chocolate Bars to retain structural integrity up to 26°C without compromising smooth in-mouth melting properties.
We offer comprehensive packaging solutions including tight-wrap foil with printed 250gsm SBS cardboard sleeves, pillow flow-wrapping, metalized barrier pouches, food-grade tins, and luxury rigid gift boxes. Our design team provides dieline templates and artwork prepress checks at zero additional cost.
Every shipment from Karachi Port is issued with a complete regulatory packet: Certificate of Analysis (CoA), Halal Certification, Commercial Invoice, Packing List, Bill of Lading, Certificate of Origin, Health/Sanitary Certificate, and detailed ingredient/allergen breakdown sheets formatted to your destination country's food safety standard.
Elevate your retail product line with high-margin, expertly crafted Nutty Chocolate Bars directly from our Lahore facility.
31-Km Ferozpur Road, Lahore, 54000, Punjab, Pakistan
+92 321 875 6419
Monday – Sunday · 10:00 – 22:00 (PKT, UTC+5)
FOB Karachi Port · EXW Lahore · CIF Destinations
English · Urdu · Arabic Written Correspondence