Knowledge Center · Candy House

Confectionery Insights & News

Industry trends, private label manufacturing guides, and export knowledge from our Lahore workshop.

0%

China has become an important manufacturing base for premium chocolate products, including Dark Chocolate Hazelnut Bars. This introduction explores what reliable production involves beyond attractive packaging. It considers ingredient sourcing, roasting methods, chocolate formulation, factory controls, and export preparation.

Experienced manufacturers usually begin with carefully selected hazelnuts, cocoa ingredients, and suitable sweeteners. Hazelnuts should offer a clean aroma, crisp texture, and consistent size. Proper roasting can create deeper flavor without producing excessive bitterness. Dark chocolate requires balanced cocoa intensity, sweetness, and smooth mouthfeel. Small adjustments matter.

Factory expertise is equally important. A professional production line should monitor temperature, mixing time, molding, cooling, and sealing conditions. Metal detection, allergen controls, sanitation procedures, and batch records support dependable quality. Independent laboratory testing may verify microbiological safety, nutritional information, and shelf-life performance. Compliance requirements can differ between destination markets, so documentation deserves early attention.

Packaging also influences product protection and customer perception. A well-sealed wrapper helps defend the bars against moisture, heat, and flavor loss. Clear labeling should identify ingredients, allergens, net weight, origin, and storage guidance. Buyers may request customized recipes, private labels, carton designs, or different bar sizes.

Not every factory delivers the same result. Supplier claims should be checked through samples, audits, certifications, and production evidence. A polished website is not enough. Taste matters. Details matter.

Some manufacturers may need to improve communication, lead-time accuracy, or consistency between sample and mass production. That weakness should be acknowledged, not hidden. Careful evaluation helps importers select a China Dark Chocolate Hazelnut Bars manufacturer that combines practical experience, technical knowledge, transparent processes, and dependable service.
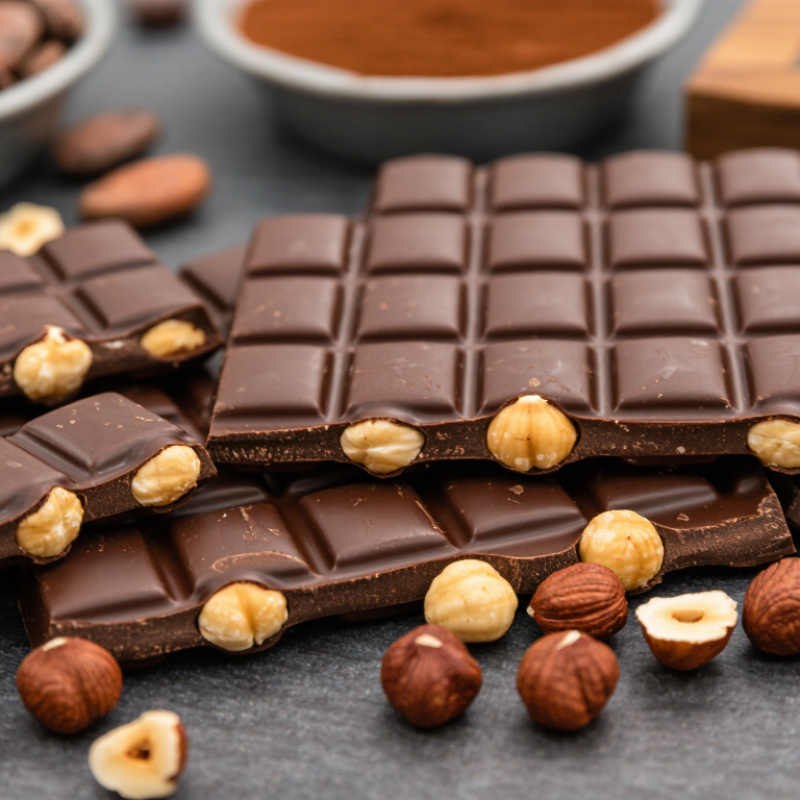
China Top Dark Chocolate Hazelnut Bars Manufacturer

Definition and Product Profile of a Dark Chocolate Hazelnut Bar Manufacturer

A dark chocolate hazelnut bar manufacturer is more than a confectionery factory. It develops, sources, produces, and verifies bars with consistent specifications. In China, an experienced manufacturer may manage cocoa liquor, cocoa butter, sugar, and roasted hazelnuts through controlled production stages. Product development begins with a clear profile: firm snap, smooth melt, and a roasted nut finish. A typical bar may contain 55% to 75% cocoa solids, depending on the intended bitterness. Hazelnut pieces should remain crisp, not soft or greasy. Small details matter. Moisture control matters too. The manufacturer should record supplier batches, roasting temperatures, allergen controls, and finished-bar weights. These records support traceability and practical quality decisions.

During production, technicians monitor tempering curves, cooling time, bar thickness, and seal quality. A well-tempered bar looks glossy and breaks with a clean sound. Operators also inspect the cut surface for uneven nut distribution. Laboratory checks can include microbiological screening, allergen verification, moisture measurement, and shelf-life observation. Packaging should protect the chocolate from heat, light, oxygen, and rough transport. Food-grade inner film and sturdy cartons are common choices. Not every trial works. A darker formula can taste too dry, while extra hazelnuts may weaken the bar. That feedback should change the next batch. Honest manufacturers keep approved samples, production records, and corrective-action notes. They also explain minimum order quantities, customization limits, and expected lead times clearly. Reliability is built through repeatable evidence, not impressive wording.

Key Ingredients and Quality Standards for Dark Chocolate Hazelnut Bars

For a China-based dark chocolate hazelnut bars manufacturer, quality begins with measurable ingredients. Cocoa mass, cocoa butter, sugar, and roasted hazelnuts should have approved specifications and supplier records. Codex Standard 87-1981 identifies key cocoa requirements for chocolate categories, including cocoa solids and cocoa butter levels. A higher cocoa percentage can create deeper flavor, but it may also increase bitterness and reduce consumer acceptance.

Hazelnuts need a clean aroma, even color, and a crisp bite. Moisture, peroxide value, aflatoxin, and foreign-material checks should appear on every lot certificate. The International Cocoa Organization estimated a 478,000-tonne cocoa deficit for the 2023/24 season. This pressure makes origin records and traceable purchasing more important. Yet traceability alone cannot fix poor roasting. Each batch needs controlled roasting, cooling, and storage. Small errors become obvious after enrobing.

Production teams should monitor particle size, viscosity, tempering curves, and finished-bar snap. Allergen segregation is essential because hazelnuts require clear control throughout the facility. HACCP and ISO 22000-based systems can support documented risk management, while destination-market rules must be checked separately. A visually perfect bar can still contain stale nuts. That is the uncomfortable weakness. Specifications should be reviewed through sensory tests, laboratory results, and customer feedback, not copied from old templates.

Manufacturing Process from Hazelnut Selection to Finished Bars

China Top Dark Chocolate Hazelnut Bars Manufacturer

Manufacturing dark chocolate hazelnut bars begins with careful nut selection. We inspect each shipment for size, freshness, aroma, and visible defects. Hazelnuts are then cleaned, calibrated, and gently roasted. Roasting develops a warm flavor without burning the delicate oils. Temperature and time are recorded for every batch. A few nuts may still roast unevenly. That is why trained operators check samples by sight and taste.

The roasted hazelnuts are cooled before controlled grinding or portioning. Dark chocolate is prepared with measured cocoa solids, sugar, and cocoa butter. We refine the mixture until its texture feels smooth on the tongue. Tempering follows, using precise heating and cooling stages. This creates a clean snap, stable shine, and better resistance to blooming. The hazelnuts are folded into the chocolate evenly. No shortcuts here.

The mixture enters bar molds, where vibration removes air pockets. Bars are cooled, inspected, and wrapped in food-grade packaging. Quality teams verify weight, appearance, texture, and traceability records. Production rooms are monitored for hygiene, temperature, and humidity. We also review customer feedback after shipment. Sometimes a bar breaks too easily or feels less nutty than expected. We adjust the process, but improvement is never finished. Reliable manufacturing depends on repeatable controls and honest review.

China Top Dark Chocolate Hazelnut Bars Manufacturer: Manufacturing Process from Hazelnut Selection to Finished Bars

This chart presents typical operating temperatures used in dark chocolate hazelnut bar production. Hazelnuts are commonly roasted at a higher temperature to develop flavor, while dark chocolate is melted, refined, tempered, molded, and cooled within controlled temperature ranges. Actual parameters vary according to recipe, equipment, particle size, and product specifications.

Packaging, Storage, and Food Safety Requirements

China Top Dark Chocolate Hazelnut Bars Manufacturer

Packaging, Storage, and Food Safety Requirements

Dark chocolate hazelnut bars need packaging that controls moisture, oxygen, light, and odor transfer. A practical structure often combines food-grade inner film with a strong outer carton. Each seal should resist tearing and remain closed during transport. Hazelnuts are major allergens, so ingredient details and allergen statements must be accurate and easy to read. Batch codes support traceability from roasting to finished packing.

Clean production areas require controlled personnel movement, equipment sanitation, and documented temperature checks. Hazard analysis should address nut contamination, foreign materials, microbial risks, and undeclared ingredients. Metal detection and seal inspections add useful protection, but neither replaces trained staff. Records should be reviewed, not merely stored. Small errors can remain unnoticed.

Storage conditions affect texture and appearance. Keep bars in a dry, dark room near 15–20°C, with stable humidity and good air circulation. Avoid direct sunlight, heating pipes, and strong-smelling products. Refrigeration may cause condensation when bars return to room temperature. During shipping, temperature loggers can reveal heat exposure that ordinary inspection misses. In practice, one carton may look perfect while its inner bars soften or develop fat bloom. Packaging tests should include vibration, stacking pressure, and warm-weather transport. Some suppliers still test only the finished appearance, which is not enough.

China Top Dark Chocolate Hazelnut Bars Manufacturer - Packaging, Storage, and Food Safety Requirements

Control Area Requirement or Specification Recommended Control Data Verification and Food-Safety Notes
Primary Packaging Use a food-contact-approved inner wrap, such as aluminum foil, metallized film, or a suitable multilayer laminate. Packaging should provide strong protection against moisture, oxygen, light, odors, and fat migration. Confirm compliance with the food-contact requirements of the destination market and retain supplier declarations of compliance.
Secondary Packaging Use clean, dry cartons that protect bars from crushing, abrasion, contamination, and temperature fluctuations during transport. Cartons should be suitable for the declared case count and pallet configuration. Use packaging materials that are odor-free and do not transfer contaminants to the chocolate or inner wrapper.
Packaging Seal Integrity Every bar should have a continuous, secure seal without holes, open edges, wrinkles at the seal, or product trapped in the sealing area. Perform routine seal checks during start-up, changeover, and production runs. Record inspection results and isolate products from any batch with compromised packaging.
Storage Temperature Store finished dark chocolate hazelnut bars in a cool, stable environment away from direct sunlight and heat sources. Recommended: approximately 15–18 °C; avoid prolonged exposure above 20 °C. Use calibrated temperature data loggers for warehouses and temperature-sensitive shipments. Product-specific validation remains necessary.
Relative Humidity Prevent condensation and moisture absorption, which may cause sugar bloom, texture changes, or packaging deterioration. Recommended: below 50% relative humidity where practicable. Do not move cold product directly into warm, humid areas without allowing controlled acclimatization.
Warehouse Hygiene Keep storage areas clean, dry, ventilated, pest-controlled, and free from chemicals, strong odors, and non-food materials. Store cartons on pallets or shelving, with clearance from walls and floors. Apply documented cleaning, pest-control, stock-rotation, and corrective-action procedures.
Allergen Declaration Declare hazelnut as a tree-nut allergen. Also declare milk or soy when used or present according to the destination-market rules. Maintain an ingredient statement and an allergen-control matrix for every formula and production line. Control cross-contact through validated cleaning, segregation, scheduling, labeling, and verification activities.
Microbiological Safety Use approved raw materials and hygienic processing controls to manage Salmonella and other microbiological hazards. Apply a risk-based sampling plan to cocoa ingredients, hazelnuts, finished products, and environmental surfaces. Low-moisture chocolate products can support long shelf life, but low water activity does not eliminate pathogen-control requirements.
Foreign-Material Control Control metal, glass, stones, hard plastics, and other physical hazards from ingredients, equipment, and packaging. Use sieving, magnets, visual inspection, and validated metal detection or X-ray inspection where appropriate. Document challenge tests, reject verification, equipment checks, and corrective actions.
Chemical and Contaminant Control Assess cocoa, hazelnuts, sugar, dairy ingredients, and other inputs for relevant contaminants and residues. Risk-assess cadmium, mycotoxins, pesticide residues, heavy metals, cleaning chemicals, and mineral-oil contaminants. Apply the legal limits and testing requirements of the importing country; limits can vary by product category and jurisdiction.
Labeling and Traceability Include product name, ingredient list, allergen declaration, net quantity, lot code, date marking, storage instructions, and responsible food-business information as required. Use a unique lot or batch code linked to ingredients, processing records, packaging materials, and distribution records. Verify label artwork against the destination-market regulations before printing or shipment.
Shelf-Life Validation Establish shelf life through documented studies rather than using a standard period for every recipe or package. Evaluate taste, aroma, texture, bloom, rancidity, packaging integrity, moisture, and microbiological quality under intended storage conditions. Use real-time testing and, where justified, accelerated studies supported by product-specific evidence.
Transport Conditions Protect finished bars from heat, rain, condensation, direct sunlight, strong odors, pests, and rough handling. Use clean, dry vehicles or containers and avoid mixed loads with chemicals or odor-emitting goods. Review temperature records and packaging condition at dispatch and receipt, especially during warm-weather shipping.
Food-Safety Management Operate under Good Manufacturing Practices and a documented HACCP-based food-safety plan. Cover hazard analysis, supplier approval, personnel hygiene, sanitation, allergen management, process controls, recall, and corrective actions. Maintain training records, monitoring logs, verification records, internal audits, and documented product-recall procedures.

How to Evaluate a Reliable China-Based Manufacturer

China Top Dark Chocolate Hazelnut Bars Manufacturer

Choosing a reliable China-based manufacturer requires more than comparing prices. Examine factory experience, production capacity, and quality systems. Request a virtual or independent factory audit. Check whether production areas look clean, organized, and properly controlled. A trustworthy supplier should explain cocoa sourcing, hazelnut processing, allergen controls, and ingredient storage clearly.

Ask for recent certificates, laboratory reports, and batch traceability records. Useful systems may include HACCP, ISO 22000, or BRCGS certification. However, a certificate alone proves little. Verify its validity and scope. Request samples from different production batches. Compare flavor, texture, bar weight, snap, and packaging strength. I would also test the product after several weeks in warm, humid conditions. Chocolate can look excellent at first and still develop surface bloom later.

Tips: Confirm minimum order quantities, lead times, carton dimensions, and payment terms in writing. Ask how damaged cartons are handled. Discuss hazelnut allergen statements and labeling requirements for your target market. Keep communication records and approve a final specification sheet before production. One overlooked detail can cause expensive rework. A cautious buyer should also review the manufacturer’s response when a sample fails. Fast, honest correction is often more valuable than polished sales language. No factory is perfect, and early questions may reveal weaknesses that a showroom will not show.

FAQS

What defines a reliable dark chocolate hazelnut bar manufacturer?

It controls sourcing, production, testing, and traceability. Each batch should have recorded ingredients, temperatures, weights, and inspection results. Clear evidence matters more than impressive wording.

What cocoa content is common in these bars?

A typical bar contains 55% to 75% cocoa solids. Higher cocoa content creates stronger bitterness. Too much darkness may taste dry, so formula trials need honest review.

How are hazelnuts prepared before mixing?

Hazelnuts are checked for size, freshness, aroma, and visible defects. They are cleaned, calibrated, and gently roasted. Operators record roasting temperature and time. Some pieces may roast unevenly.

How does tempering affect the finished bar?

Controlled heating and cooling create a glossy surface and clean snap. Tempering also improves resistance to fat bloom. Cooling time and temperature require careful monitoring. No shortcuts here.

How are hazelnuts distributed evenly?

Roasted nuts are cooled before portioning or folding into chocolate. Bar molds may use vibration to remove air pockets. Inspectors check the cut surface for uneven nut distribution.

What packaging protects dark chocolate hazelnut bars?

Food-grade inner film and strong cartons help block moisture, oxygen, light, and odors. Seals should resist tearing during transport. Vibration, stacking, and warm-weather tests reveal weaknesses.

How should the bars be stored?

Store them near 15–20°C in a dry, dark room. Keep humidity stable and air circulation adequate. Keep them dry. Avoid sunlight, heating pipes, and strong-smelling goods.

What food safety controls are important?

Controls should cover sanitation, personnel movement, foreign materials, microbial risks, and undeclared ingredients. Hazelnuts require clear allergen statements. Metal detection helps, but trained staff remain essential.

How can buyers evaluate production reliability?

Request approved samples, batch records, traceability information, and corrective-action notes. Ask about minimum orders, customization limits, and lead times. Records should be reviewed, not merely stored.

Conclusion

A China-based dark chocolate hazelnut bar manufacturer specializes in producing chocolate bars that combine refined cocoa flavor with the rich, crunchy texture of roasted hazelnuts. High-quality Dark Chocolate Hazelnut Bars depend on carefully selected cocoa ingredients, fresh hazelnuts, suitable sweeteners, and controlled formulations that meet consistent standards for taste, texture, appearance, and cleanliness. The manufacturing process generally includes hazelnut inspection and roasting, chocolate preparation, ingredient blending, molding, cooling, and final quality testing.

Reliable packaging should protect the bars from moisture, heat, light, and physical damage during storage and transportation. Manufacturers should also maintain hygienic production areas, traceable raw materials, documented quality controls, and appropriate food safety procedures. When evaluating a China-based supplier, buyers should review production capabilities, ingredient sourcing, testing systems, customization options, packaging services, lead times, and communication efficiency. A dependable partner should provide stable quality, transparent processes, flexible support, and products that match the buyer’s market and application requirements.
Amelia

Amelia

Amelia is a professional marketing specialist dedicated to helping customers better understand the value, quality, and practical benefits of the company’s products. With extensive knowledge of product features, customer needs, and market trends, she creates clear, informative, and engaging content......