Confectionery Insights & News
Industry trends, private label manufacturing guides, and export knowledge from our Lahore workshop.
High-Performance Packaging & OEM Product Solutions
Explore our validated product capabilities ranging from food-grade barrier films and precision label rolls to specialty confectionery formulations and custom cosmetic containers.
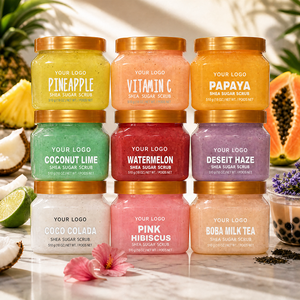
Private Label Wholesale Organic Shea Butter Sugar Body Scrub Coco Exfoliating Salt Hydrating For Stretch Marks All Skin Types
High-barrier moisture-resistant jar packaging designed for organic formulations. Ensures extended product stability and shelf protection.
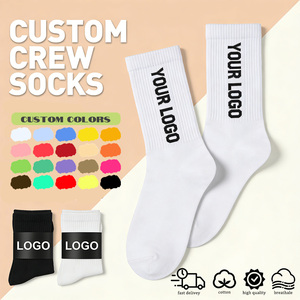
High Quality Design Logo Socks Men Customised Branded Cotton Socks Wholesale Crew Breathable Personalized Custom Socks
Bespoke retail packaging solutions including printed header cards, band wraps, and custom display boxes for apparel merchandising.
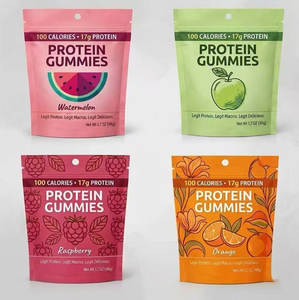
Customized High Protein Gummy Supplier for Gym and Sports Nutrition Muscle Recovery Energy Booster
Nutraceutical-grade starch-moulded gummies packaged in nitrogen-flushed pouch packaging for optimized active ingredient longevity.
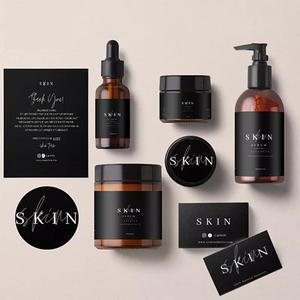
Custom Printed Cosmetic Bottle Makeup Product Packaging Adhesive Paper Logo Label Sticker
Precision CMYK printing with oil and water-resistant synthetic stocks, tailored for cosmetic bottles and food-grade containers.
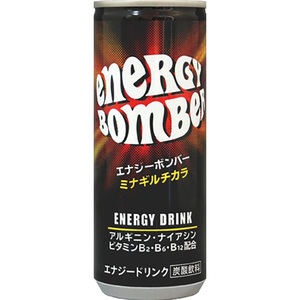
Aseed Energy Bomber Japanese Fantastic Taste Private Label Caffeine 250ml Can Natural Drink
Standardized aluminum beverage can packaging engineered for pressurized carbonated and functional caffeine drinks.
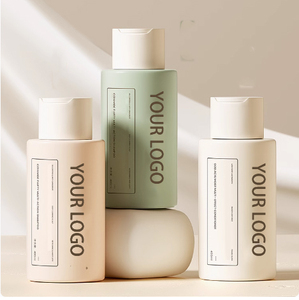
Skin Care Products Customized Private Label Natural Organic Plant Ingredients Deep Cleansing Hair Shampoo and Conditioner Set
Custom PET/HDPE bottle sets featuring precision pump dispensers and high-durability branding for personal care lines.
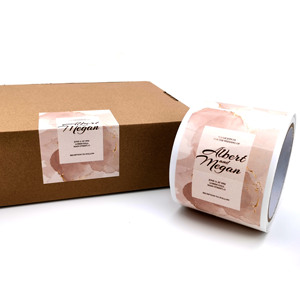
Custom Private Packaging Label Product Sticker Printing Adhesive Brand Logo Round Label Rolls Waterproof Vinyl Sticker
Industrial-grade automated label rolls compatible with high-speed packaging machinery, offering anti-scratch vinyl coatings.
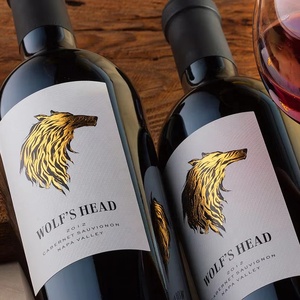
Wholesale Custom Private Labels Waterproof Beverage Bottles with CMYK Printing Custom Size & Shape for Whisky & Wine
Bespoke die-cut waterproof labels with foil accents for premium wine, spirits, and glass bottle confectionery syrup lines.
Top 10 Candy Packaging Factory Criteria
Evaluating global confectionery packaging facilities requires analyzing barrier engineering, throughput efficiency, material compliance, and supply chain reliability. Here are the core benchmark metrics defining elite manufacturers.
| Packaging Tier / Material Spec | Primary Confectionery Application | Moisture & Oxygen Barrier Rating | Recyclability & Eco Profile | Standard MOQ Range |
|---|---|---|---|---|
| Metallized BOPP / PE Laminates | Flow-wrap hard candies, chocolate bars, toffees | Ultra-High (WVTR < 0.3g, OTR < 0.5cm³) | Standard Multi-layer Recycling Stream | 300 kg / Film Roll Run |
| Mono-Material Recyclable PE | Gummy pouches, jellies, chewy candies | High (WVTR < 0.8g, OTR < 1.5cm³) | 100% Circular Economy Recyclable | 500 kg / SKU |
| Rigid 1200 GSM Setup Boxes | Ramadan, Eid, Christmas & Luxury Gifting Sets | Structural Mechanical Protection | FSC-Certified Biodegradable Board | 1,000 Units |
| Pectin & Gelatine Blister Trays | Single-serve gummies, functional pastilles | Hermetic Thermoformed Seal | Recyclable PET/RPET Trays | 5,000 Strips |
| Lithographed Tinplate Packaging | Premium truffles, mints, hard candies | Complete Light, Air & Moisture Block | Infinite Metal Recyclability | 2,000 Tins |
Evaluating the World's Top 10 Candy Packaging Factories
In global food manufacturing, candy packaging is far more than outer branding—it is an active barrier system engineered to prevent sugar bloom, fat migration, oxidative rancidity, and atmospheric moisture degradation.
1. Barrier Science & Shelf-Life Extension
Top candy packaging facilities utilize co-extruded substrates to combat water vapor transmission rate (WVTR) and oxygen transmission rate (OTR). For gelatine gummies and moisture-sensitive starch confections, inadequate barrier properties lead to stickiness or stoving reversal. Advanced factories integrate aluminum oxide (AlOx) coatings or EVOH barrier layers to safeguard texture without compromising transparency.
2. Cold-Seal vs. Heat-Seal Flow Wrapping
For high-speed chocolate bar wrapping, heat-sealing creates thermal degradation that melts cocoa butter at the package margins. Leading packaging factories deploy cold-seal adhesive technologies (natural rubber latex formulations) that bond instantly under pressure alone, enabling packaging line speeds exceeding 1,200 individual bars per minute while preserving product tempering integrity.
3. Regulatory Compliance & Halal Protocols
Confectionery export markets throughout the GCC, Southeast Asia, and Europe mandate strict food contact materials (FCM) compliance. Elite packaging plants maintain dedicated cleanroom environments certified under ISO 22000, HACCP, and BRCGS. Crucially, release agents, printing inks (low-migration UV/water-based inks), and laminating adhesives must be certified Halal and free from animal-derived fatty acids.
Key Information Gain Insight for B2B Procurement Managers
When sourcing from candy packaging factories, requesting a certificate of analysis (CoA) for solvent retention is paramount. Residual solvent levels in flexographic or gravure printed films must remain below 5 mg/m² to prevent off-odor migration into delicate milk chocolate lipid matrices.
Why International Buyers Partner With Our Manufacturing Base
Headquartered at 31-Km Ferozpur Road, Lahore, Pakistan, Candy House (Private) Limited integrates confection formulations with high-end structural packaging design under a single quality control framework.
Small-Batch & High-Volume Flexibility
Unlike rigid mega-factories requiring container-load minimums per single flavor, our 40kg to 250kg batch-cook system allows buyers to consolidate mixed SKUs—chocolates, sour jellies, and hard candies—into single consolidated shipments.
Equatorial Thermal Guard Shipping
Exporting chocolate and jelly products through warm transit corridors demands specialized packaging staging. We formulate specific fat-bloom inhibitors and configure thermal container liners for all FOB Karachi shipments between November and March.
Complete In-House Packaging Design
From rigid 1200 gsm hot-foil stamped gift boxes for Ramadan and Eid to automated CMYK waterproof roll labels for liquid syrups and candy jars, our design team produces print-ready dielines and pre-production proofs in-house.
Future Procurement & Packaging Trends (2025–2030)
The confectionery packaging landscape is shifting rapidly due to environmental regulations, consumer demand for clean labels, and retail automation. Strategic procurement directors are prioritizing four main developments.
Mono-Polymer Circular Recyclability
Multi-layer laminates combining PET, aluminum foil, and PE are being phased out across European and North American markets due to recycling restrictions. Future-proof factories are transitioning to orientation-boosted mono-PE and mono-PP film structures that maintain high-barrier oxygen ratings while fitting 100% into standard curbside recycling streams.
Active & Smart Humidity Control
Integrations of desiccant-embedded inner film matrices and moisture-indicating inks allow real-time monitoring of confectionery freshness across global cold chains. This reduces product returns driven by ambient humidity spikes during tropical ocean freight.
Biodegradable Paper-Based Flow Wraps
Replacing traditional plastic candy wrappers with barrier-coated paper substrates is becoming standard for organic and premium dark chocolate brands. High-durability water-dispersible dispersion coatings provide adequate fat resistance while ensuring marine degradability within 180 days.
Frequently Asked Questions by B2B Buyers
Clear answers regarding custom packaging production, minimum order volumes, lead times, and dietary certifications.
What is the minimum order quantity (MOQ) for custom private label candy packaging?
Private label production starts at 300 kg per recipe for gummies and starch jellies, and 500 kg per SKU for moulded chocolate bars. First-time buyers can request a 100 kg trial validation run to assess retail shelf velocity prior to initiating full container-load (FCL) orders.
How do you ensure chocolate wrappers do not melt products during shipping?
We deploy cold-seal adhesive packaging lines that eliminate heat zones near the chocolate during wrapping. Additionally, we coordinate reefer container logistics and install insulated thermal blankets for sea freight routes originating from Karachi Port during warm climate seasons.
Are all candy packaging materials compliant with Halal and food contact standards?
Yes. All raw film stocks, paperboard, laminating adhesives, and printing inks (water-based and low-migration UV inks) are certified 100% Halal and compliant with US FDA and EU Regulation No 1935/2004 for direct food contact.
What is the typical lead time from design approval to dispatch?
Standard catalogue items ship within 12 to 18 working days post artwork approval. Bespoke confectionery recipes requiring custom injection moulds, tin embossing dies, or specialized rigid box tooling take approximately 25 to 35 working days.
Can we consolidate mixed candy categories into a single shipping container?
Absolutely. Because our manufacturing facilities produce chocolates, hard candies, gummies, marshmallows, and printed packaging solutions under one roof, buyers can combine multiple SKUs into a single 20ft or 40ft container to optimize freight costs per kilogram.
Ready to Elevate Your Confectionery Packaging & OEM Lines?
Request our comprehensive product catalog, technical barrier data sheets, and competitive FOB/CIF quotation tailored to your market requirements.