Confectionery Insights & News
Industry trends, private label manufacturing guides, and export knowledge from our Lahore workshop.
Export-Ready OEM & Private Label Product Solutions
Direct factory contract manufacturing, custom formulation, turn-key packaging, and specialized labeling solutions for global distributors and retail brands.
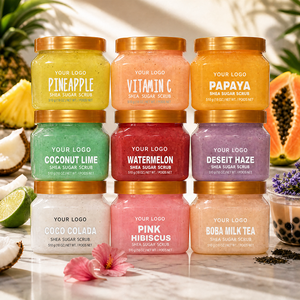
Organic Shea Butter Sugar Exfoliating Scrub
High-viscosity organic formulation designed for stretch mark reduction and deep hydration across all skin types.
Contact Us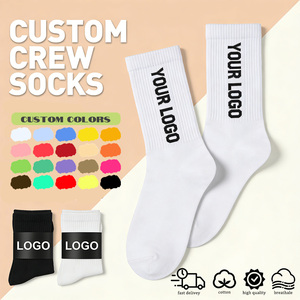
Custom Branded Breathable Cotton Crew Socks
200-needle high-density knit combed cotton socks with bespoke jacquard logo integration for brand promotions.
Contact Us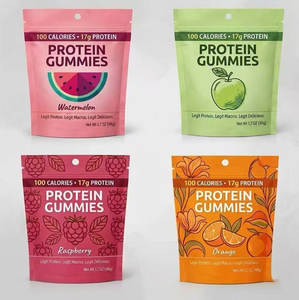
Sports Nutrition High Protein Energy Gummies
Fortified amino acid and whey isolate gummy matrix engineered for muscle recovery, sports nutrition, and stamina.
Contact Us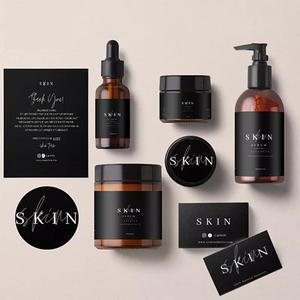
Adhesive Custom Packaging Stickers & Bottle Labels
Waterproof vinyl and metallic foil pressure-sensitive labels customized for cosmetics and retail bottles.
Contact Us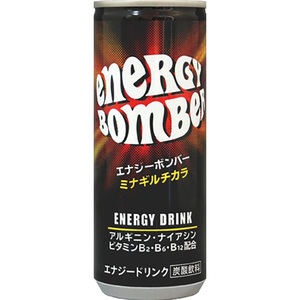
Caffeinated Energy Bomber 250ml Aluminum Can
Pasteurized carbonated energy beverage featuring natural caffeine extracts and targeted B-vitamin complex.
Contact Us
Organic Botanical Hair Shampoo & Conditioner Set
Sulfate-free plant extract formulation for scalp nourishment, hair follicle strength, and deep cleansing.
Contact Us
High-Precision CMYK Round Packaging Label Rolls
Rotary die-cut waterproof roll stickers engineered for high-speed automated packaging machines.
Contact Us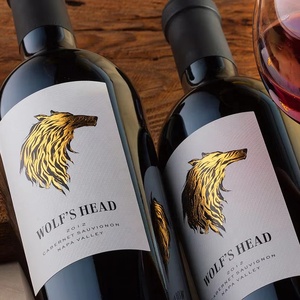
Custom Waterproof Labels for Wine & Spirits Bottles
Condensation-resistant adhesive film labels featuring textured embossing and gold leaf hot-stamping.
Contact UsIndustrial Strategic Blueprint: Navigating Global OEM/ODM Confectionery Contracts
The global contract manufacturing landscape for confectionery, functional gummies, and custom-branded packaging has undergone a structural paradigm shift. Today’s international buyers—ranging from institutional food distributors and pharmacy chains to high-velocity private-label brands—require far more than standard sugar-boiling capabilities. Modern procurement demands rigorous scientific stability, precise Brix control (78–80°), verifiable thermal shelf-life under extreme ambient conditions, strict Halal/HACCP compliance, and fully integrated turn-key packaging operations.
As an established manufacturing authority operating from our state-of-the-art facility at 31-Km Ferozpur Road, Lahore, Pakistan, Candy House (Private) Limited bridges the gap between artisanal small-batch quality control and industrial OEM production scalability. This comprehensive whitepaper explores the critical technical parameters, ingredient engineering trends, global supply chain risks, and regulatory frameworks required to build high-margin, high-repeat private label confectionery portfolios in 2025 and beyond.
Why Institutional Buyers Partner With Our Lahore Facility
Direct technical communication with food technologists, in-house packaging engineers, and controlled batch processing.
Controlled Starch-Tray Curing
Unlike low-cost operations using 8-hour rapid setting, our jellies and gummies undergo a 48–72 hour slow-cure process in climate-controlled starch trays.
- Optimal elastic bite & non-sticky surface finish
- Eliminates melting risk during tropical sea freight
- Custom bloom strength (180 to 250 Gelatin/Pectin)
Bean-to-Bar Chocolate Hall
Equipped with 250 kg/day tempering capacity, in-house roasting, and stone-conching units for single-origin and custom milk/dark chocolate blends.
- Strict cocoa butter crystallization monitoring
- Heat-stable formulations up to 26°C transit limit
- Zero palm-oil adulteration options available
Turn-Key Packaging & Labeling
Integrated rotary die-cut roll printing, flow-wrapping, nitrogen-flushed pouches, and rigid box manufacturing under one central production management floor.
- Full food-grade compliance (FDA & EU standards)
- Waterproof vinyl & hot-foil printing capabilities
- Automated high-speed barcode & lot tracking
Future Procurement Trends in Confectionery Contracting
Market shifts shaping B2B contract manufacturing, active ingredient encapsulation, and sustainability mandates.
1. The Functional Gummy Explosion & Nutraceutical Integration
The boundary between traditional confectionery and health supplements has permanently dissolved. Institutional buyers are shifting procurement allocations toward fortifiable gummy bases capable of carrying heat-sensitive active ingredients including Whey Isolate, Creatine, Vitamin D3, Electrolytes, and Probiotics. Key technical challenges involve maintaining active potency while masking bitter botanical profiles without destroying texture. Factories offering specialized low-temperature syrup depositing will dominate the high-margin pharmacy and sports nutrition sectors over the next decade.
2. Plant-Based Pectin & Sugar-Reduced Formulations
Global consumer demand is accelerating away from animal-derived gelatine toward citrus pectin and modified starches. Modern B2B buyers require formulations tailored for Vegan, Kosher, and Halal-conscious demographics simultaneously. Furthermore, sugar-reduced recipes substituting sucrose with isomalt, maltitol, or natural erythritol require precise moisture activity control ($a_w < 0.60$) to prevent crystallization and moisture migration during international container transport.
3. Thermal Stability & Warm-Climate Logistics Engineering
Climate volatility and container transit delays across major shipping lanes (such as Karachi to the Gulf, EU, or North America) have elevated thermal stability to a primary vendor selection metric. Importers are rejecting suppliers whose products deform at ambient temperatures above 22°C. Contract factories are investing in structural hydrocolloid matrixing and protective wax/oil polishing coats that withstand temp spikes up to 32°C without clumping.
4. Integrated Packaging & Full Lot Traceability
B2B buyers no longer accept split vendor models where candy is manufactured at one site and shipped elsewhere for custom labeling. Unified contract facilities that handle high-speed roll label printing, tamper-evident barrier seals, and automated carton packing cut lead times by 40%. Additionally, continuous digital batch tracking—from raw ingredient certificate to final sea-freight container seal—is now mandatory for top-tier retail compliance.
OEM/ODM Manufacturing Specification Matrix
Comprehensive operational parameters across key production lines at Candy House (Pvt) Ltd.
| Product Category | Minimum Order Quantity (MOQ) | Technical / Recipe Specs | Packaging Options | Shelf-Life & Stability |
|---|---|---|---|---|
| Functional & Sports Gummies | 300 kg / Recipe | Pectin or Gelatine base; 78–80° Brix; Fortified with Protein/Caffeine/Vitamins | Stand-up barrier pouches, PET Jars, 1kg bulk bags | 12 Months @ 18–22°C, RH < 55% |
| Handcrafted Tempered Chocolates | 500 kg / SKU | 70% Dark, Milk, or White; Pure cocoa butter; Roasted whole nuts | Aluminium foil inner + printed sleeve, rigid luxury gift boxes | 12 Months (Dark/Milk); 9 Months (White) |
| Hand-Pulled Hard Candies & Swirl Pops | 400 kg / SKU | 148°C High-cook sugar syrup; Natural or nature-identical flavorings | Individual cello-wrap, printed stick tags, display tubs | 24 Months (Low moisture moisture activity $a_w$) |
| Custom Labeling & Packaging Rolls | 2,000 Roll Units | Waterproof PP/PET vinyl; CMYK + Spot UV; Hot foil stamping | Automatic application roll cores (76mm standard) | Indefinite under dry indoor storage |
| Soft Aerated Marshmallows & Toffees | 250 kg / SKU | Whipped gelatin matrix; Low-density foam structure; Butter toffees | Nitrogen-flushed pillow packs, lithographed keepsake tins | 9–12 Months in airtight barrier film |
Frequently Asked Questions for B2B Importers & Brands
Direct answers to technical, regulatory, and logistics inquiries managed by our engineering department.
Q1: What is the standard minimum order quantity (MOQ) for custom private label gummies?
Standard private-label production begins at 300 kg per recipe for pectin or gelatine-based gummies. For first-time global importers who need retail trial validation before committing to a full 20ft container, we offer pilot trial runs starting at 100 kg per recipe with semi-custom packaging options.
Q2: How does your factory handle heat sensitive chocolate and gummy shipments to warm climates?
We engineer recipes specifically for target destination climates. Gummy lines utilize optimized pectin hydrocolloid structures with high solid Brix levels (78–80°) to prevent melting. Chocolate exports shipped between April and October utilize refrigerated reefer containers (18°C constant temperature control) with temperature logging strips placed inside every sea-freight pallet.
Q3: Are all production lines strictly certified Halal and HACCP compliant?
Yes. Candy House (Private) Limited operates under a 100% Halal-certified facility framework in Lahore, Pakistan. All gelatine sourced is strictly certified bovine Halal. We operate a documented HACCP food safety protocol with automated inline metal detectors and sieve filtration across every boiling and depositing line.
Q4: Can you assist with packaging artwork die-lines and custom label printing?
Extensively. Our in-house structural packaging team provides complete dieline templates, artwork pre-press checks, barcode verification, and nutrition label calibration according to destination market regulations (FDA, EU, GCC GSO standards). We print high-resolution roll labels, pouches, and rigid boxes under the same roof.
Q5: What is the typical lead time from deposit payment to port dispatch?
Standard catalog recipes with customer artwork dispatch within 12 to 18 working days post artwork approval. Bespoke recipes requiring custom brass moulds or unique active ingredients take 25 to 35 working days. Transit from Karachi Port reaches Arabian Gulf ports in 7–10 days, European hubs in 22–28 days, and North American ports in 30–38 days.
Q6: Do you support consolidation of mixed confectionery categories in a single container?
Yes. Because our plant manufactures cooked hard candies, starch-moulded jellies, tempered chocolate, and aerated marshmallows at one unified campus (31-Km Ferozpur Road, Lahore), buyers can consolidate multiple product SKUs into a single 20ft or 40ft container to optimize freight costs.
Ready to Scale Your Private Label Confectionery Line?
Consult directly with our food technologists and OEM project managers today. Request sample kits, custom recipe quotes, or plant audits for your next procurement cycle.
Contact Us