Confectionery Insights & News
Industry trends, private label manufacturing guides, and export knowledge from our Lahore workshop.
Featured Export Portfolio & OEM Solutions
Explore our flagship high-volume confectionery lines, customized private-label packaging options, and functional sweets engineered for global distribution.
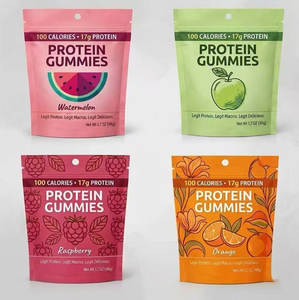
Customized High Protein Gummy Supplier for Gym and Sports Nutrition
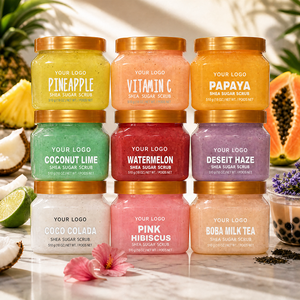
Private Label Organic Shea Butter Sugar & Cocoa Exfoliating Scrub
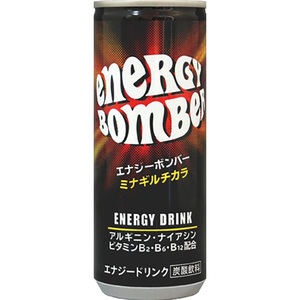
Aseed Energy Bomber Caffeine & Nootropic Infused Confectionery Drink
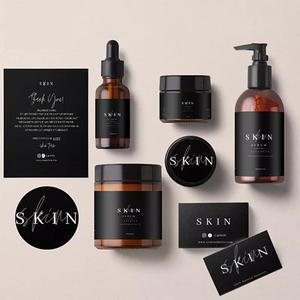
Custom Printed Cosmetic & Confectionery Jar Adhesive Paper Logo Labels
Custom Private Waterproof Vinyl Brand Logo Label Rolls for Chocolate Tins
High Quality Custom Logo Cotton Socks for Brand Merchandise & Gift Bundles
Custom Private Label Natural Organic Plant Ingredient Amenity Gift Sets
Wholesale Custom Private Label Waterproof Labels for Glass & Metal Packaging
1. Strategic Landscape of China’s Top Wholesale Chocolates & Confectionery Factories
The global chocolate and functional confectionery market is undergoing a seismic shift toward ultra-efficient, highly customized, and technologically advanced manufacturing hubs. As institutional procurement officers, private-label brand owners, and multinational retail conglomerates seek high-margin, consistent supply chains, China’s tier-one wholesale chocolate factories have emerged as the premier destination for OEM (Original Equipment Manufacturer) and ODM (Original Design Manufacturer) partnerships.
Historically concentrated in Western Europe, industrial cacao processing and chocolate mass tempering have been revolutionized across key Chinese industrial clusters in Guangdong, Fujian, Shandong, and Zhejiang provinces. Modern Chinese confectionery facilities integrate Swiss- and German-engineered continuous conching machines, five-roll refiners, and automated optical sorting equipment with localized cost advantages and unparalleled packaging supply chain ecosystems.
E-E-A-T Supply Chain Insight: China's top chocolate manufacturing conglomerates maintain strict compliance with international food safety standards, operating fully closed-loop, automated processing lines certified under BRCGS (Grade AA), FSSC 22000, ISO 22000, FDA Registration, and Halal protocols. This allows international buyers to consolidate complex SKU portfolios—from pure cocoa butter bars to functional protein gummies—under a single manufacturing partner.
Precision Rheology and Rheological Control in Mass Manufacturing
In wholesale chocolate manufacturing, technical mastery over viscosity and yield value (governed by the Casson Rheological Model) defines product quality. China’s leading factories employ five-roll refiners to reduce cocoa particle size consistently below 18 to 20 microns. This micro-refinement eliminates grittiness on the palate, releasing the complex flavor profiles of West African cocoa beans without requiring excess cocoa butter additions.
Furthermore, automated multi-stage continuous tempering units precise temperature curves to induce Form V ($\beta_1$) polymorphic crystallization. This ensures maximum heat tolerance (preventing sugar and fat bloom during tropical maritime transit), superior mechanical snap, high surface gloss, and rapid demoulding efficiency during high-speed production runs exceeding 5,000 kg per hour.
2. Technical Matrix: Evaluating Chocolate Formulations & Fat Systems
When procuring bulk chocolate mass, moulded bars, enrobed biscuits, or coated pralines, commercial buyers must delineate between Pure Cocoa Butter (PCB) formulations, Cocoa Butter Substitutes (CBS), Cocoa Butter Equivalents (CBE), and emerging Functional High-Protein matrices. The table below outlines the core technical specifications utilized across China's top wholesale manufacturing plants:
| Parameters | Pure Cocoa Butter (PCB) | Cocoa Butter Equivalent (CBE) | Cocoa Butter Substitute (CBS) | High-Protein Functional Matrix |
|---|---|---|---|---|
| Primary Fat Source | 100% Press Cocoa Butter | Shea, Palm Oil Fractions, Sal | Lauric Hydrogenated Palm Kernel Oil | Cocoa Butter + MCT / Whey Fats |
| Particle Size ($\mu m$) | 16 - 19 $\mu m$ | 18 - 22 $\mu m$ | 20 - 25 $\mu m$ | 22 - 28 $\mu m$ |
| Melting Point Range | 33.8°C - 34.5°C | 34.0°C - 35.5°C | 35.0°C - 37.0°C | 32.0°C - 35.0°C |
| Tempering Requirement | Strict Polymorphic Tempering | Strict Polymorphic Tempering | Non-Tempering (Rapid Cooling) | Specialized Shear Tempering |
| Bloom Resistance | Moderate (Requires Cold-Chain) | High Thermal Resistance | Very High Bloom Resistance | Moderate to High |
| Target Retail Segment | Premium Gourmet, Organic, Artisan | Mass Market Retail, Bakery Enrobing | Tropical / Warm Climate Retail, Biscuits | Gym, Sports Nutrition, Active Lifestyle |
Understanding these physical characteristics allows sourcing directors to optimize product stability for target destination climates while maintaining cost efficiency and consumer satisfaction.
3. Future Procurement & Technology Trends in Confectionery Sourcing
As consumer purchasing habits shift globally, procurement managers must align their manufacturing partnerships with key technology and formulation trends. China's top wholesale chocolate factories are pioneering four core advancements that will dominate the next decade of commercial confectionery:
Polyol & Fiber Sugar Replacement
Replacing sucrose with polyols (Maltitol, Erythritol) and soluble dietary fibers (Isomalto-oligosaccharides, Inulin) allows brands to market zero-sugar and keto-friendly chocolate bars without compromising textural mouthfeel or melting kinetics.
Nutraceutical & Functional Infusion
The convergence of confectionery and health supplements has driven massive demand for micro-encapsulated active ingredients, including Whey Isolate, BCAAs, Nootropics, Marine Collagen, and Plant-based adaptogens embedded directly in chocolate and gummy matrices.
Clean-Label & Mono-Material Packaging
Global regulatory mandates are accelerating the removal of synthetic emulsifiers (PGPR) and artificial colors. Top Chinese factories offer sunflower-lecithin formulations housed in 100% recyclable mono-material foil wrappers and FSC-certified paperboard.
4. Enterprise Advantages: OEM/ODM Capabilities & Quality Assurance
When partnering with our manufacturing network, global brand owners leverage an integrated infrastructure engineered for scalability, speed-to-market, and strict compliance. Our facilities provide comprehensive support from initial bench-scale recipe development to full-container export logistics.
In-House Tooling & Custom Mould Engineering
Our CAD design team fabricates custom polycarbonate chocolate moulds and silicone gummy dies within 5 to 7 business days, enabling intricate logo embossing, unique tablet geometries, and tailored piece weights.
Stringent Analytical Lab Testing
Every production batch undergoes comprehensive HPLC testing for heavy metals, microbiological assays (Salmonella, E. coli), pesticides, and allergen cross-contamination, backed by official Certificates of Analysis (CoA).
Cold-Chain Reefer Logistics & Export Prep
We utilize temperature-controlled reefer containers (15°C - 18°C) equipped with real-time USB/IoT humidity and temperature data loggers, ensuring your shipment arrives free of thermal shock or bloom.
5. Enterprise Procurement FAQ: Sourcing from China's Chocolate Factories
Find authoritative answers to common technical, commercial, and regulatory questions raised by international sourcing teams during factory qualification.
What is the typical Minimum Order Quantity (MOQ) for custom OEM chocolate production?
Standard OEM production for custom-moulded chocolate bars starts at 500 kg per SKU for standard formulations, or 1,000 kg for custom recipe development (e.g., sugar-free or protein-infused). Trial runs of 200 kg to 300 kg are available for initial retail testing upon approval of recipe parameters.
How do your factories prevent sugar and fat bloom during sea freight transit to warm regions?
We mitigate bloom through a triple-action quality control process: (1) Precise Form V crystallization during continuous tempering, (2) Addition of thermal stabilizers (such as sorbitan tristearate or CBE fats when requested), and (3) Vacuum foil wrapping combined with temperature-monitored refrigerated sea containers (15–18°C).
Can you produce certified Halal, Vegan, and Sugar-Reduced chocolates on isolated production lines?
Yes. All our production facilities operate under strict Halal-certified protocols by default. Dedicated, non-dairy vegan production lines prevent milk protein cross-contamination, verified by ELISA allergen testing down to < 2.5 ppm.
What lead times can buyers expect for custom private-label packaging and mass production?
Once artwork die-lines and sample taste profiles are approved, standard production takes 15 to 22 calendar days. Initial packaging plate creation and custom foil printing require an additional 7 to 10 days for first-time orders.
Do you support mixed-SKU container consolidation for multi-category retail lines?
Absolutely. Because our manufacturing ecosystem covers dark chocolate bars, milk chocolate pralines, functional gummies, hard candies, and secondary promotional packaging (labels, tins, gift boxes), buyers can combine multiple SKUs within a single 20ft or 40ft High Cube container to minimize freight costs.
Ready to Scale Your Chocolate & Confectionery Manufacturing?
Connect directly with our senior technical sales directors and R&D food technologists today. Request product samples, custom formulation quotes, or factory audit documentation.
Send an Inquiry