Confectionery Insights & News
Industry trends, private label manufacturing guides, and export knowledge from our Lahore workshop.
Featured Export-Grade Confectionery & OEM Solutions
Explore our highly requested contract-manufactured product lines, private-label packaging, and functional chocolate formulations tailored for global markets.
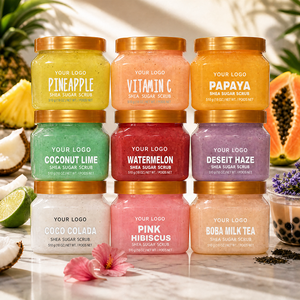
Custom Private Label Shea & Cocoa Butter Formula Solutions
High-purity cocoa butter and natural botanical formulation capability. Engineered for precise melting control, premium texture, and custom export packaging.
Send an Inquiry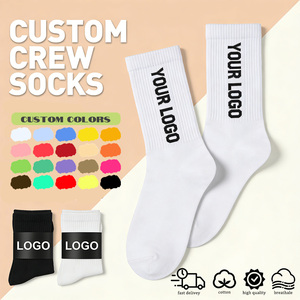
High-Quality Custom Branded Corporate Apparel & Merchandising
Full-spectrum corporate identity solutions accompanying bulk food exports. Custom logo printing, breathable cotton items, and promotional packaging sets.
Send an Inquiry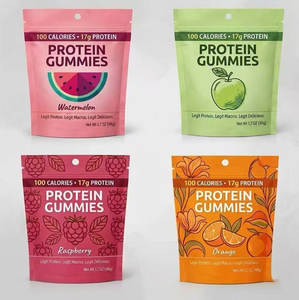
Customized High Protein Gummy & Functional Energy Booster
Advanced functional nutrition lines for sports performance, muscle recovery, and energy enhancement. Formulated with stable active ingredients and low-sugar bases.
Send an Inquiry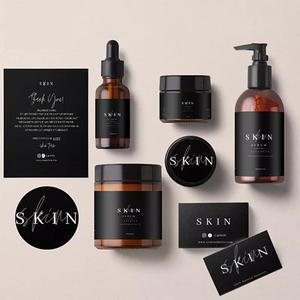
Custom Printed Packaging Adhesive Logo Labels & Roll Stickers
Waterproof, high-tack foil and vinyl custom labels for retail confectionery boxes, bottles, and display cartons. Precision CMYK & Pantone matching.
Send an Inquiry
Private Label Natural Caffeine Energy & Functional Beverage Lines
Automated canning and bottling line capabilities for natural caffeine, botanical extracts, and functional refreshment drinks designed for international distribution.
Send an Inquiry
Custom Organic Botanical Extract Formulation & Packaging
Clean-label organic manufacturing standards using sustainably sourced plant lipids, essential oils, and food-grade bio-active components.
Send an Inquiry
Custom Waterproof Vinyl Brand Logo Round Labels & Seals
High-durability product sealing labels designed to withstand humidity and cold-chain shipping environments without peeling or color fading.
Send an Inquiry
Wholesale Waterproof CMYK Foil Labels for Premium Packaging
Bespoke embossing, metallic gold foil stamping, and specialty adhesive die-cut labels engineered for luxury chocolate boxes and retail bottles.
Send an InquiryThe Evolution of China's Chocolate Manufacturing Infrastructure
Over the past two decades, China’s industrial confectionery sector has undergone a profound technological metamorphosis. Once dominated by basic compound sugar coating processes, contemporary Chinese chocolate manufacturers now stand at the apex of global bean-to-bar and mass-scale automated chocolate bar production. Driven by multi-million-dollar investments in European-engineered continuous tempering technology, micro-refining conches, and ISO-class cleanroom enrobing facilities, China has emerged as a preferred manufacturing partner for international brands, retail chains, and wholesale distributors seeking uncompromised quality paired with supply chain efficiency.
Modern B2B chocolate procurement is no longer solely about unit cost reduction; it demands strict adherence to international food safety benchmarks (HACCP, ISO22000, BRCGS, Halal, Kosher), precise Rheological behavior control, yield stress consistency, and thermal stability for transcontinental logistics. Chinese manufacturers are now leveraging state-of-the-art five-roll refiners that reduce particle size below 18 microns (µm), delivering a velvety mouthfeel that rivals traditional Swiss and Belgian confectioners while offering unprecedented flexibility in custom OEM formulations.
Emerging B2B Sourcing & Manufacturing Trends (2025–2030)
Global buyer preferences in the chocolate bar ecosystem are shifting rapidly towards clean labels, nutritional enhancement, and ethical transparency. Procurement directors must align their supply chains with these pivotal market trends:
Chocolate is expanding beyond indulgence into functional wellness delivery. Leading Chinese manufacturers are integrating high-protein whey/plant isolates, botanical adaptogens, probiotic strains, and dietary fiber into dark and milk chocolate matrices without disturbing crystal formation or flavor release profile.
With global sugar-reduction mandates expanding, B2B buyers are procuring chocolate bars sweetened with Allulose, Erythritol, Stevia, and Monk Fruit. Precision crystallization techniques ensure these alternative sugars do not cause bloom or unpleasant cooling aftertastes.
Utilizing micro-milled oat flour, coconut milk solids, and almond lipids, modern Chinese ODM plants are creating vegan milk chocolate bars that replicate the exact creamy profile and snap of classic dairy formulations for eco-conscious demographics.
Traceability is paramount. Premium exporters in China offer fully verified supply chains, sourcing cocoa beans directly from West Africa (Ivory Coast, Ghana), Ecuador, and domestic Hainan origins with Rainforest Alliance and Fairtrade compliance certificates.
Chocolate Bar Formulation & Manufacturing Capability Matrix
A comparative standard guide for international procurement managers evaluating OEM/ODM manufacturing protocols.
| Parameter / Grade | Pure Cocoa Butter (Craft/Premium) | Cocoa Butter Equivalent (CBE) | Compound Chocolate (CBR/CBS) |
|---|---|---|---|
| Fat Source | 100% Deodorized & Natural Cocoa Butter | Cocoa Butter + Shea/Palm Fractions | Hydrogenated Palm Kernel Oil |
| Melting Profile | Sharp melt at body temperature (36°C) | Near-identical to pure cocoa butter | Higher melting point (38°C–42°C) |
| Particle Size (Finishing) | < 18 microns (Ultra-Smooth) | 18 – 22 microns | 22 – 25 microns |
| Tempering Requirements | Strict Form V Beta Crystal Control Required | Requires tempering process | Non-tempering, rapid cooling set |
| Thermal Stability | Requires Temperature Control (18–22°C) | Moderate Heat Resistance | High Heat Stability for Tropical Zones |
| Target Retail Segment | Boutique Brands, Specialty Grocery, Gift Sets | Mass Retail, Confectionery Snacks | Value Snacks, Enrobing, Baking Lines |
| MOQ Range (Private Label) | 500 kg per SKU | 1,000 kg per SKU | 2,000 kg per SKU |
China's Leading Manufacturing & Export Core Advantages
Integrating deep industry heritage, automated production lines, and client-centric custom packaging solutions.
Our manufacturing facility houses fully automated Buhler continuous refining, Aasted tempering systems, and high-speed Bosch wrapping equipment capable of producing over 150 metric tons of finished chocolate bars daily with zero human contamination risk.
We offer total customization—from custom-engraved chocolate bar moulds with your brand logo to high-barrier inner aluminum foil wrapping, rigid presentation boxes, and recyclable paper sleeves created by our dedicated in-house structural design team.
Shipping delicate chocolate globally requires flawless supply chain management. We utilize thermal-insulated container liners, gel refrigerant packs, and real-time IoT temperature monitoring from our warehouse in China direct to your port of destination.
Every production lot undergoes rigorous laboratory testing including atomic absorption spectrometry for heavy metals, microbial culture analysis, fat bloom resistance stress tests, and automated X-ray metal detection prior to container loading.
To assist growing brands and market testing, we offer scalable trial order protocols starting at just 300 to 500 kg per custom recipe, allowing retail validation before scaling up to full 20ft/40ft container loads.
Our products are exported seamlessly across North America, Europe, the Middle East, and Southeast Asia. We supply full documentation sets including Health Certificates, Certificates of Analysis (COA), FDA Registrations, Halal, and Kosher certifications.
Frequently Asked Questions for Chocolate Procurement
Detailed answers to critical technical, logistical, and commercial queries from international importers and procurement officers.
What is the baseline Minimum Order Quantity (MOQ) for custom private-label chocolate bars?
For standard catalog recipes utilizing existing bar moulds (such as 80g or 100g standard formats) with custom-printed outer paper packaging, our baseline MOQ starts at 500 kg per SKU. For fully customized bar shapes requiring bespoke CNC copper mould production, the initial MOQ is 1,000 kg. We also offer pilot batch sampling runs (100–200 kg) for market validation upon formal commercial evaluation.
How do you prevent chocolate fat bloom and melting during ocean freight through tropical transit zones?
Fat bloom occurs when polymorph V cocoa butter crystals transform into polymorph VI due to temperature fluctuations. We prevent this through three engineering layers: First, precisely controlled seeding tempering during enrobing to ensure 100% Stable Form V beta crystals. Second, formulation adjustments using natural vegetable fats (in CBE options) or milk fat fractions to elevate melt thresholds. Third, export logistics utilizing reefer containers (set strictly at 15°C–18°C) or thermal foil insulation blankets inside standard dry containers with continuous temperature logging sensors.
Can your factory produce certified Halal, Vegan, and Sugar-Free chocolate bar lines?
Yes. Our facility maintains dedicated cleanroom production shifts and isolated raw material storage to guarantee zero cross-contamination. Our Halal-certified lines comply with JAKIM and GSO standards. For vegan and plant-based contracts, we eliminate all dairy derivatives, substituting with oat milk solids or coconut lipids. Sugar-free ranges utilize pure maltitol, erythritol, or monk fruit, fully supported by glycemic index test reports and nutrition labeling compliance for target market regulations.
What is the standard production lead time and sample turnaround period?
Custom lab samples for recipe and flavor approval require 5 to 7 working days. Once taste profiles and packaging dielines are signed off by the buyer, full-scale mass production takes 18 to 25 calendar days. For custom mould engineering, add 10 business days for CNC mould fabrication and testing. Ocean transit times vary by port: 7–12 days to Southeast Asia, 15–22 days to Middle Eastern ports, 22–30 days to Europe, and 25–35 days to North America.
What packaging materials are available for export chocolate bars?
We offer comprehensive primary and secondary packaging options: Primary wraps include food-grade heat-sealable aluminum foil, eco-friendly compostable cellulose film, and cold-seal flow wrapping. Secondary options include 250–350 gsm art paper sleeves with foil stamping, metallic embossing, matte/gloss lamination, display counter boxes (CDUs), tinplate gift boxes, and rigid cardboard presentation packages.
How is raw material quality guaranteed across large-scale continuous orders?
We enforce strict lot-by-lot Quality Assurance protocols. All cocoa liquor, cocoa butter, and cocoa powder inputs undergo HPLC analysis for purity, moisture testing (<1.5%), fat content verification, and microbiological screening (Salmonella, E. Coli, Listeria). During refining, particle size is verified every 2 hours with laser diffraction analyzers. Final finished products are retained in climate-controlled sample libraries for the entirety of their stated shelf life (typically 12 to 24 months).
Ready to Launch Your Premium Chocolate Bar Product Line?
Partner with China's leading contract chocolate manufacturer. Request factory-direct pricing, custom formulation consultation, and free sample kits tailored to your brand's market requirements today.